Sterility Testing
Checking for microbial contamination, such as bacteria and fungi.
From the manufacturing environment and quality testing to lot management—
we apply a quality-focused lens to every stage.
HLE Medical ensures product quality through
the management of our manufacturing environment, rigorous quality testing,
and detailed record-keeping for every production lot.
A controlled manufacturing environment underpins our cell cultivation technology.
HLE Medical’s stem cell secretome is produced using Class 100 safety cabinets housed within a cleanroom environment with a cleanliness rating of Class 10,000.
Through strict hygiene and equipment management, we maintain quality control at every stage—from cell cultivation to the collection of secreted components.

Three quality tests for every production lot.
HLE Medical conducts sterility, mycoplasma, and endotoxin testing on every single production lot.
We verify product quality—specifically regarding microbial contamination and endotoxins, which cannot be detected by visual inspection alone—based on established test methods and acceptance criteria.
Checking for microbial contamination, such as bacteria and fungi.
Checking for mycoplasma contamination.
Measuring the level of bacterial endotoxins.
Managing quality information and manufacturing records for each production lot.
At HLE Medical, we manage quality information for every production lot, ensuring it is linked to the corresponding manufacturing records and test results.
We also provide quality-related documentation—such as Safety Data Sheets (SDS), Certificates of Analysis (COA), and raw material specifications—so that you can review quality information for our products.
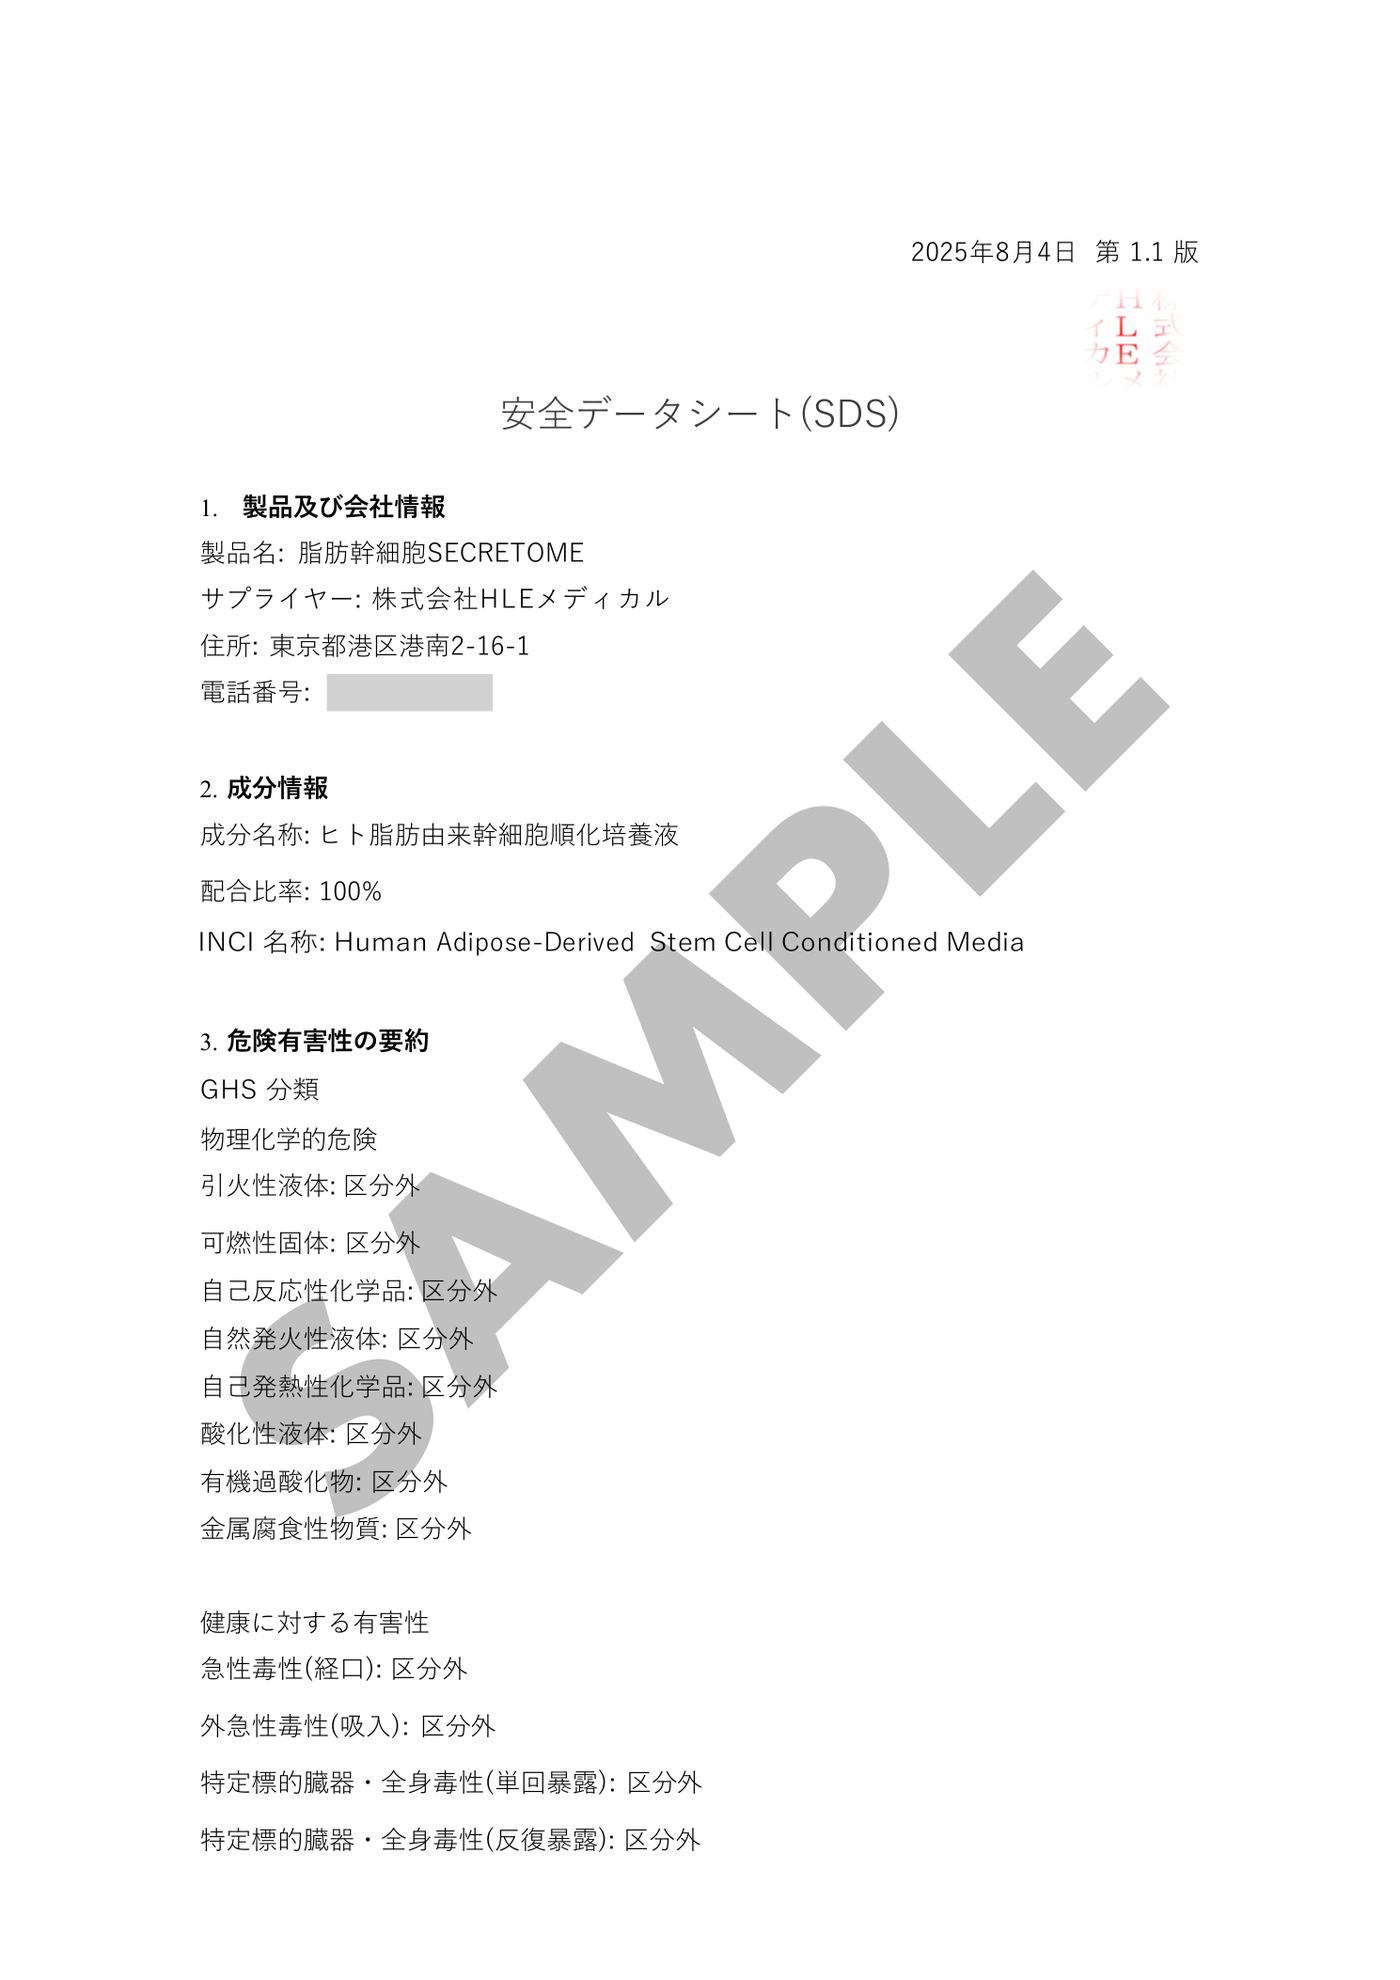
Information regarding product properties and safe handling
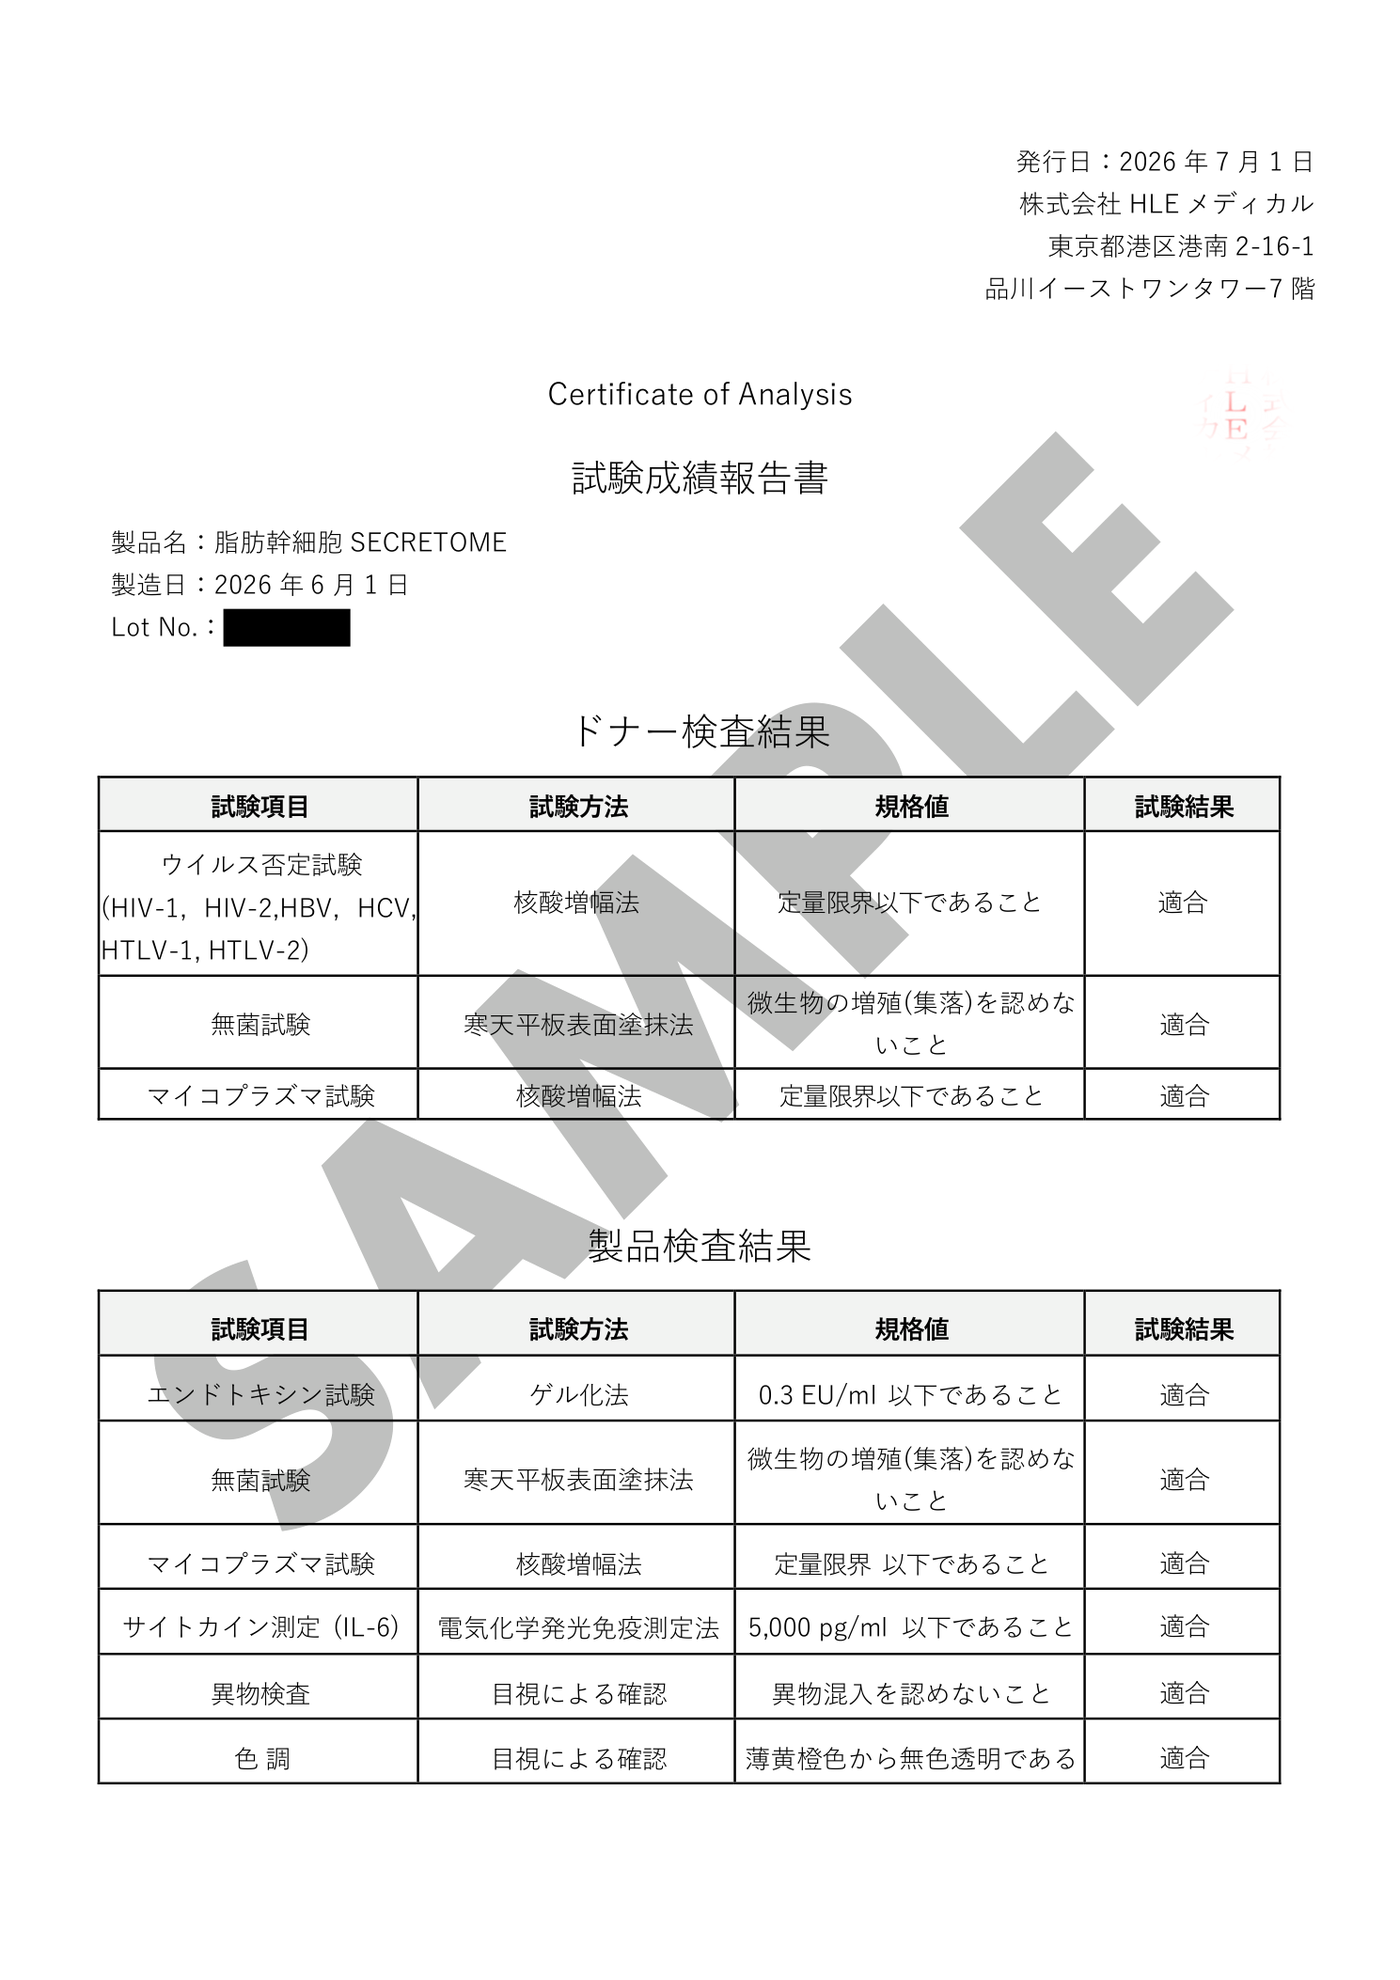
Test parameters and results for each production lot
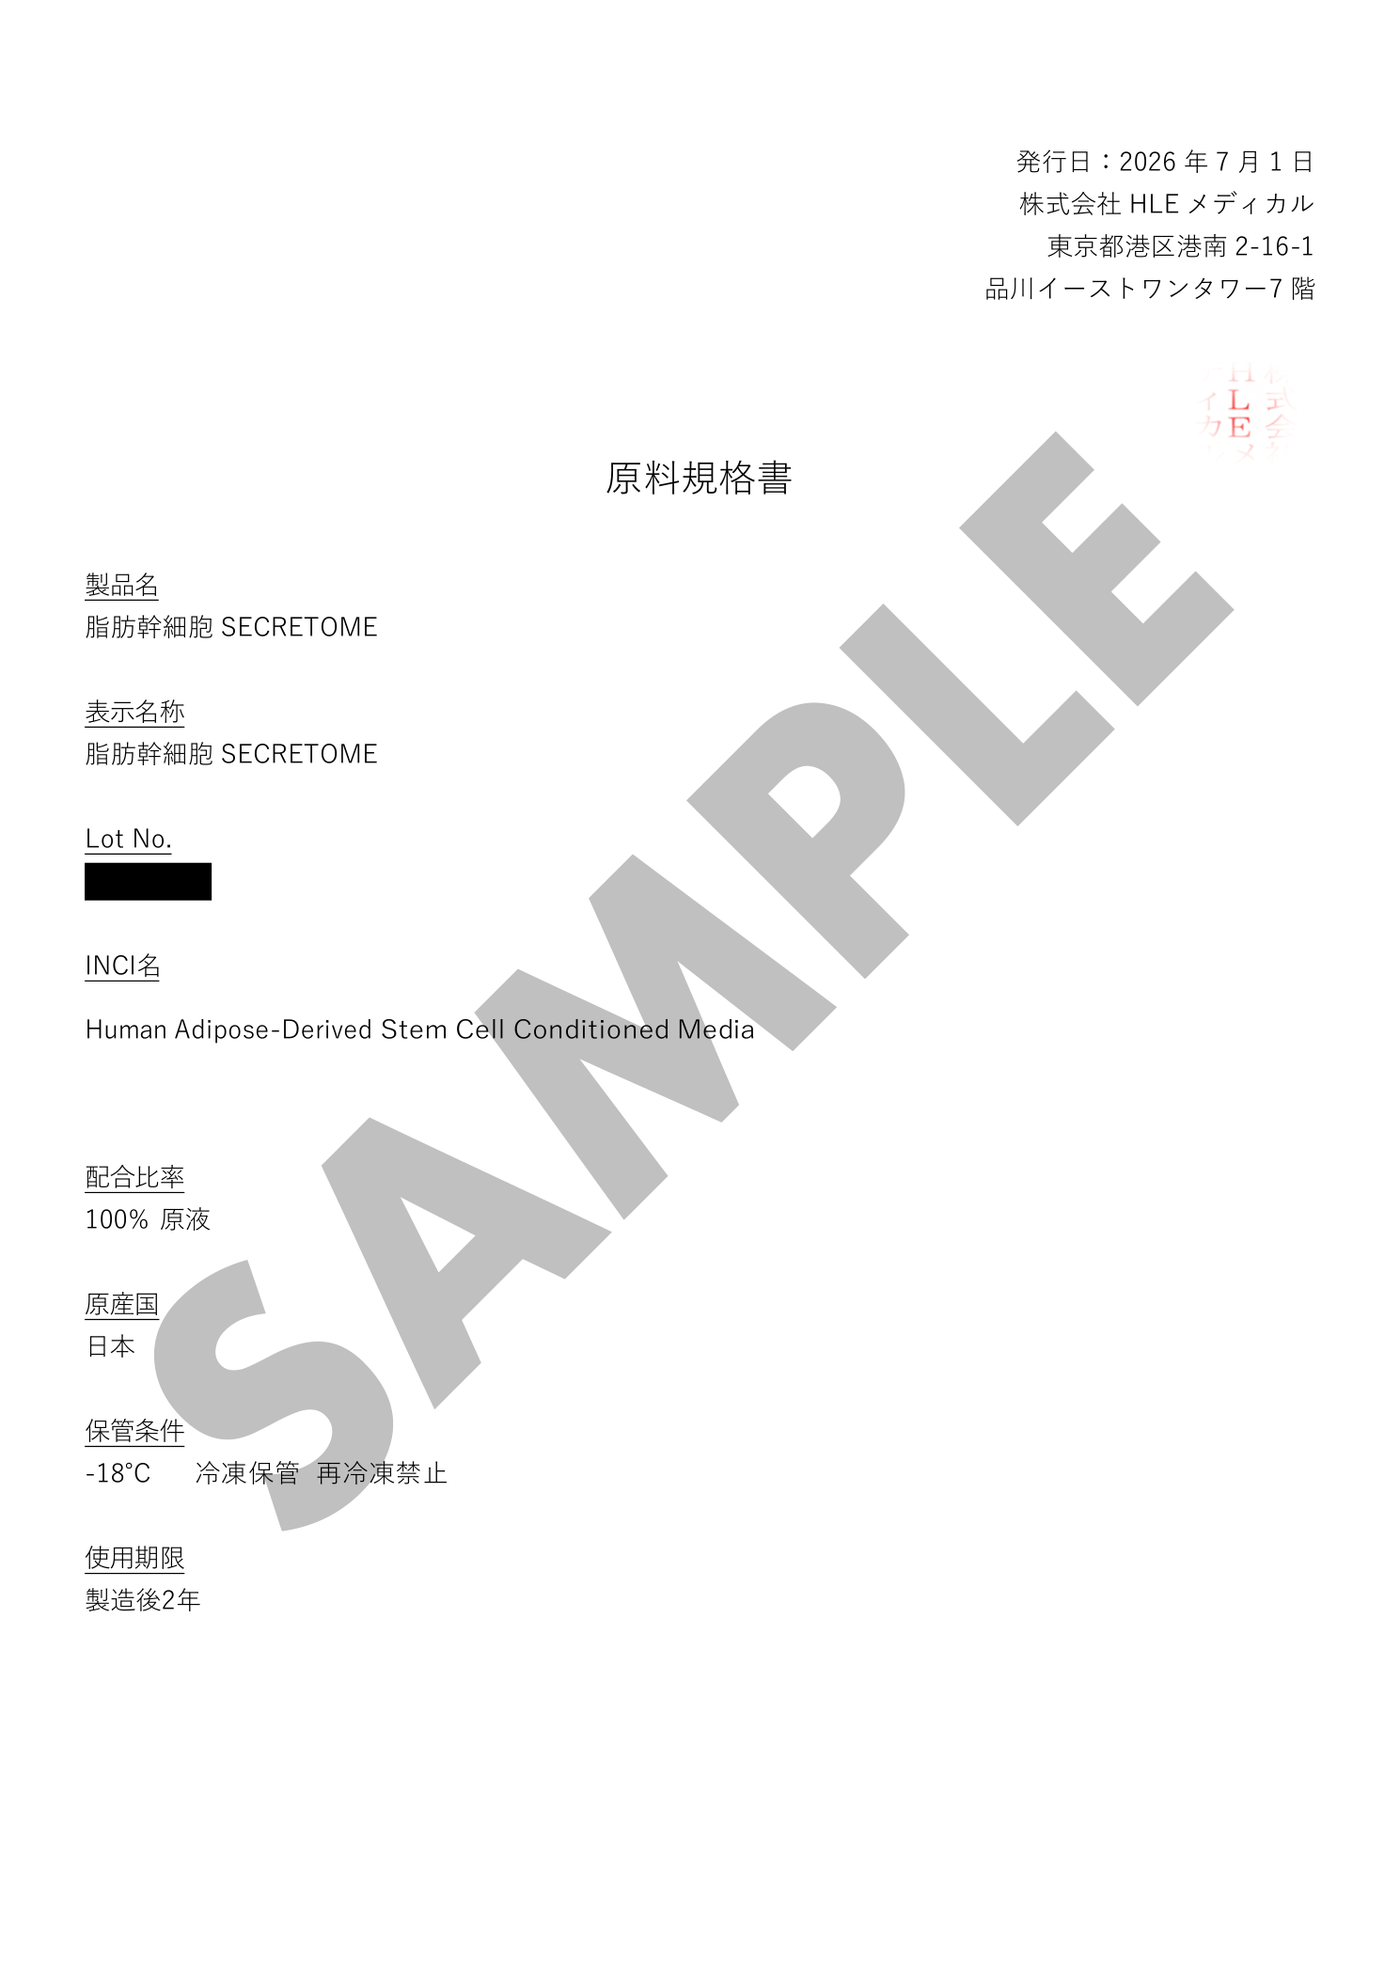
Specifications and quality standards for raw materials
*The documents shown here are samples. Please contact us for the official quality-related documentation.
Manufacturing, inspection, dispatch, and delivery.
We apply controls tailored to the specific characteristics of each product at every stage of the process.
At HLE Medical, we place great importance on quality control throughout every stage—from manufacturing and quality verification to storage and delivery.
We employ storage and delivery methods tailored to the specific characteristics of each product type (frozen or freeze-dried) and the prevailing temperature conditions.
Produced in a controlled environment
Quality testing and verification for each lot
Managed under conditions suited to product characteristics
Delivered according to specified requirements
Stored frozen at -18°C.
Shipped under specified frozen conditions.
Generally stored and shipped at room temperature.
Stored and shipped under refrigeration, depending on temperature conditions.
At HLE Medical, we provide product quality information and various quality-related documentation,
tailored to your specific needs and considerations.